A Pvc Factory is more than a building filled with mixers, extruders, and cooling tanks. It is a controlled production system that turns carefully measured raw materials into pipes, profiles, flooring, cable insulation, and other durable products. Understanding this process helps buyers judge quality beyond a polished catalog or low quoted price.
Tony Radoszewski, a longtime PVC industry executive, has stated, “PVC is a versatile material because performance depends on responsible formulation and processing.” This idea captures the factory’s real responsibility. Resin selection, stabilizers, plasticizers, pigments, and impact modifiers must work together. Small formulation errors can cause brittle surfaces, uneven color, poor dimensional stability, or premature failure.
Inside a Pvc Factory, production commonly begins with material batching and high-speed mixing. The blended compound is then heated, shaped, cooled, and cut. Extrusion lines may run continuously, while injection molding machines create precise fittings and components. Operators monitor temperature, pressure, speed, and wall thickness throughout the shift.
Quality control is not a final inspection alone. It includes incoming-material checks, sample testing, visual examination, and performance verification. Workers may test tensile strength, impact resistance, density, and dimensional accuracy. Yet no factory is perfect. Equipment drifts. Human judgment varies. Unexpected defects still appear.
That is why reliable manufacturers document each batch and investigate failures honestly. Energy use, scrap PVC, worker protection, and responsible waste handling also deserve attention. This guide examines how a Pvc Factory operates, what each production stage achieves, and where manufacturing decisions can quietly affect the finished product.
A PVC factory is a controlled production site that turns PVC resin into useful building, electrical, medical, and consumer products. Grand View Research valued the global PVC market at about USD 45 billion in 2023. Demand remains strong because PVC is durable, lightweight, and relatively economical.
The factory usually starts with PVC resin powder. Workers blend it with stabilizers, plasticizers, pigments, impact modifiers, and processing aids. Extrusion lines then heat and shape the mixture through metal dies. They produce pipes, window profiles, cable insulation, wall panels, gutters, and flexible tubing. Injection molding creates fittings, valves, containers, and small technical parts. Calendering machines make sheets, flooring layers, and artificial leather.
Products need different formulas. Rigid pipe requires strength and dimensional stability. Flexible cable coating needs controlled plasticizer levels. Medical tubing demands tighter cleanliness and testing. PlasticsEurope reported that PVC represented roughly one-tenth of European plastics production in recent industry data, showing its continuing industrial importance.
Quality teams check thickness, color, tensile strength, impact resistance, and surface defects. They also test batch consistency. Small temperature changes can affect gloss or shrinkage.
No production line is perfect.
That assumption needs testing. A factory may recycle clean internal edge trim, but contaminated material can reduce performance. Energy use also deserves attention, especially during heating and cooling. Good factories record these losses instead of hiding them.
A PVC factory converts salt, hydrocarbons, and electricity into a versatile polymer. The raw materials begin with ethylene and chlorine. Chlorine usually comes from brine electrolysis, while ethylene comes from hydrocarbon cracking. These materials form ethylene dichloride, or EDC, which is thermally cracked into vinyl chloride monomer, or VCM. According to the European Chemicals Agency’s VCM substance dossier, VCM requires closed handling because it is hazardous before polymerization. That detail matters. A factory is not simply a mixing hall.
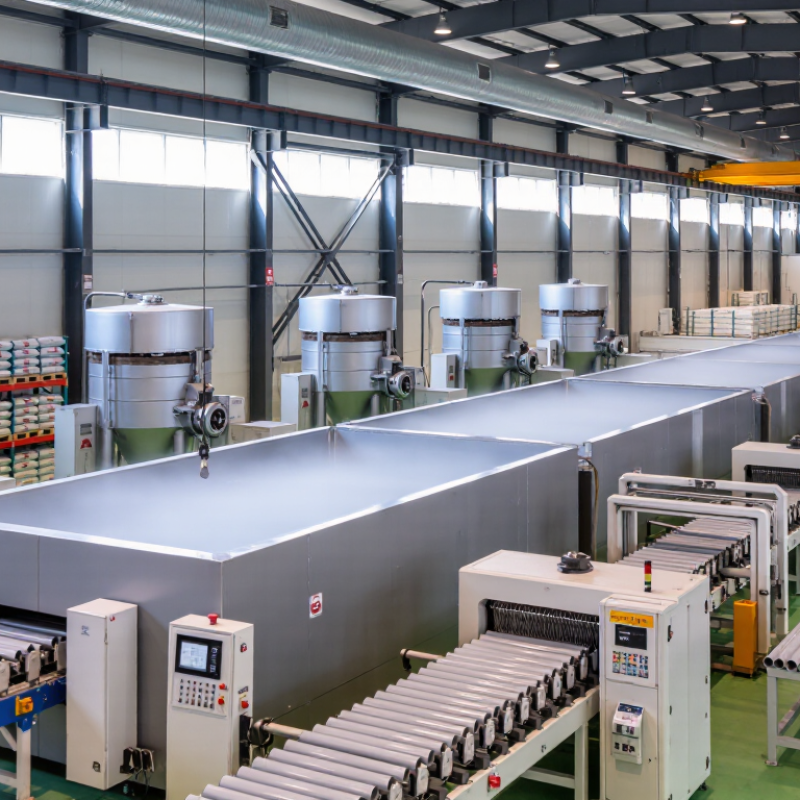
Key equipment follows the chemical sequence. Brine purification units remove calcium and magnesium before membrane electrolyzers operate. Cracking furnaces produce VCM from EDC. Distillation columns then separate unreacted materials. In suspension polymerization, jacketed reactors control temperature, pressure, and particle size. Centrifuges remove water, and fluidized-bed or hot-air dryers reduce residual moisture. Silos store the PVC resin before compounding. Extruders later blend stabilizers, plasticizers, impact modifiers, or pigments for specific products.
Energy and water use deserve close attention. The International Energy Agency identifies the chemical sector as a major industrial energy consumer, and PVC production shares that pressure through electrolysis, heating, cooling, and drying. PlasticsEurope’s Plastics—The Fast Facts 2023 report places PVC among Europe’s major polymer types, supporting its continuing industrial relevance. Yet production figures alone can mislead. A modern factory may recover VCM and process water, but imperfect maintenance still creates losses. Operators need continuous leak detection, corrosion monitoring, and independent emissions checks. Small faults can become expensive failures.
| Production Area | Raw Material or Equipment | Function | Typical Data or Operating Range | Key Considerations |
|---|---|---|---|---|
| Main Feedstock | Ethylene and chlorine | Used to produce ethylene dichloride, which is converted into vinyl chloride monomer (VCM). | Industrial PVC production generally uses a balanced chlor-alkali and ethylene-based feedstock system. | VCM is toxic, flammable, and tightly controlled, so closed handling systems are essential. |
| Polymerization Feed | Vinyl chloride monomer, water, initiator, and suspension additives | Forms PVC particles through suspension, emulsion, or bulk polymerization. | Suspension PVC is commonly polymerized in water at approximately 40–70 °C, depending on the grade and process design. | Temperature, pressure, particle size, and conversion must be carefully controlled. |
| Polymerization Equipment | Jacketed polymerization reactor | Provides mixing, heat removal, pressure control, and controlled conversion of VCM into PVC resin. | Usually equipped with an agitator, cooling jacket or coils, pressure instruments, and automated controls. | Effective heat removal is important because polymerization releases heat. |
| VCM Recovery | VCM stripping column, condenser, vacuum system, and recovery tank | Removes residual monomer from PVC slurry and recovers it for reuse. | Residual VCM in finished resin is reduced to meet applicable occupational and product-safety requirements. | Leak detection, ventilation, closed transfer, and emissions treatment are critical. |
| Solid-Liquid Separation | Centrifuge or filtration system | Separates wet PVC resin particles from process water after polymerization. | The target is a consistent wet-cake moisture level before drying. | Efficient separation reduces dryer energy consumption and wastewater load. |
| Drying and Classification | Fluid-bed dryer, hot-air dryer, cyclone, and vibrating screen | Dries PVC resin, removes fines or oversized particles, and produces a uniform powder. | Commercial PVC resin is generally dried to a low moisture level, often below approximately 0.3% depending on grade. | Airflow and temperature affect powder quality, residual moisture, and energy use. |
| Base Polymer | PVC resin powder | Provides the structural polymer matrix for pipes, profiles, cables, films, flooring, and other products. | K-value commonly ranges from about 50 to 80 for many general-purpose grades, with the exact value selected for processing and end use. | Higher K-values generally indicate higher molecular weight and can increase melt strength and processing demands. |
| Heat Stabilizer | Calcium-zinc, organotin, or other approved stabilizer systems | Reduces thermal degradation and discoloration during processing. | Dosage depends on the formulation and is commonly specified in parts per hundred resin (phr). | Selection must consider regulations, processing temperature, color stability, and end-use requirements. |
| Plasticizer | Phthalate or non-phthalate plasticizer, where permitted | Increases flexibility and softness in flexible PVC products. | Flexible formulations may contain approximately 20–100 phr or more, depending on the desired hardness and application. | Rigid PVC normally contains little or no plasticizer; regulatory limits vary by application and market. |
| Impact Modifier | Acrylic, CPE, or other compatible modifier | Improves impact resistance, particularly in rigid PVC profiles, siding, and fittings. | Typical addition levels are often in the range of approximately 2–15 phr, depending on the product. | Excessive loading can affect stiffness, fusion behavior, and surface appearance. |
| Lubricants | Internal and external lubricants, such as fatty-acid derivatives or waxes | Controls friction, fusion, melt flow, and release from metal processing surfaces. | Often used at low dosage levels, commonly below approximately 2 phr for many formulations. | The balance is important: too little may cause sticking, while too much may delay fusion. |
| Fillers and Pigments | Calcium carbonate, titanium dioxide, carbon black, and color pigments | Adjusts cost, stiffness, opacity, color, density, and surface appearance. | Calcium carbonate levels can range from low percentages to more than 50 phr in selected products. | Particle size, surface treatment, purity, and dispersion strongly affect product performance. |
| Dry Blending | High-speed hot mixer and cooling mixer | Disperses additives throughout the PVC resin and creates a consistent dry blend. | Hot mixing may discharge around 100–130 °C, followed by cooling before storage or processing. | Mixing time, sequence, temperature, and batch consistency influence fusion and final quality. |
| Compounding and Pelletizing | Twin-screw extruder, die, strand or underwater pelletizer | Melts, disperses, homogenizes, and converts the dry blend into uniform pellets. | PVC melt processing is commonly controlled within approximately 160–200 °C, depending on formulation and residence time. | Overheating can release hydrogen chloride, so temperature control and ventilation are necessary. |
| Product Forming | Pipe extruder, profile extruder, film line, cable coating line, or calender | Shapes compounded PVC into finished products such as pipes, sheets, films, profiles, and cable insulation. | Processing conditions vary by product; cooling, sizing, haul-off speed, and die design determine dimensions. | Stable melt temperature and accurate dimensional control are essential for consistent output. |
| Quality Control | Laboratory instruments and production inspection systems | Verifies resin properties, formulation consistency, dimensions, appearance, and mechanical performance. | Common checks include K-value, bulk density, moisture, particle size, hardness, tensile strength, impact resistance, and color. | Testing methods should match the intended product standard and local regulatory requirements. |
| Environmental and Safety Systems | Scrubber, wastewater treatment, dust collector, ventilation, and gas detection | Controls VCM emissions, PVC dust, hydrogen chloride, wastewater contaminants, and workplace hazards. | Systems are designed according to process capacity, emission limits, hazardous-area classification, and applicable law. | Safe PVC manufacturing requires closed systems, emergency procedures, preventive maintenance, and continuous monitoring. |
Note: Actual formulations, equipment capacities, temperatures, and additive levels vary according to the PVC grade, product design, plant scale, and applicable safety and environmental regulations.
A PVC factory converts salt, ethylene, and controlled energy into useful plastic products. PlasticsEurope’s Plastics—the Fast Facts 2023 reports 400.3 million tonnes of global plastic production in 2022. PVC represents a significant share of construction materials.
The process begins with brine electrolysis, which produces chlorine and caustic soda. A cracker supplies ethylene from hydrocarbons. Chlorine and ethylene then react into ethylene dichloride, or EDC. Heating EDC creates vinyl chloride monomer, known as VCM. This step requires sealed equipment and continuous monitoring.
VCM enters suspension polymerization tanks with water and initiators. Small PVC particles form under controlled temperature and pressure. Workers remove residual VCM, separate the polymer, and dry it. The powder then receives stabilizers, impact modifiers, pigments, or plasticizers. Extruders melt and shape the compound into pipes, profiles, films, or cables.
Tips: Check temperature records, VCM readings, and moisture levels at every shift. A clean powder is not automatically a safe product. Testing can still miss poor mixing.
The International Energy Agency notes that petrochemical demand will remain a major driver of oil and gas use. This makes energy efficiency important in PVC production. Heat recovery, closed-loop cooling, and lower-loss extrusion can reduce waste. The process looks highly controlled, yet real factories still face uneven particle size, equipment fouling, and occasional quality drift. That weakness deserves honest review.
A PVC factory turns resin, stabilizers, and other approved additives into pipes, profiles, sheets, or fittings. Quality control begins before production starts. Technicians check incoming materials against purchase specifications and test moisture, color, density, and contamination. Each batch receives a traceable code. Small errors here can affect the entire production run.
Many facilities use ISO 9001 principles to control documents, training, corrective actions, and customer feedback. Product testing may follow applicable ASTM, EN, or national standards. The exact standard depends on the product and its destination. Operators monitor melt temperature, screw speed, cooling water, and line pressure during extrusion. Calibrated gauges matter. An inaccurate gauge can hide a serious process drift.
Finished PVC products undergo dimensional checks, visual inspection, impact testing, and pressure testing when required. Pipes may also face tests for stiffness, leakage, chemical resistance, and long-term performance. Inspectors record results instead of relying on memory. Independent laboratories can verify critical samples and strengthen credibility. Still, no factory is flawless. A rushed inspection, unclear sampling plan, or poorly stored sample can weaken reliable data. Regular internal audits help expose these gaps before customers do. Workers should also have authority to stop a line when measurements move outside approved limits. That practice costs time, but it protects consistency.
A PVC factory turns resin and approved additives into pipes, profiles, sheets, or flexible products. The process usually involves weighing, mixing, heating, forming, cooling, and cutting. Each stage can create safety and environmental risks. Fine powder may irritate workers, while overheated material can release harmful fumes.
Reliable factories use enclosed mixers and local exhaust ventilation near heating equipment. Temperature sensors help prevent overheating during extrusion or molding. Workers need task-specific training, eye protection, gloves, and hearing protection. Lockout procedures are essential before cleaning or repairing machinery. Small leaks matter. Routine inspections should record dust levels, ventilation performance, machine guards, and emergency responses.
Waste management begins with accurate material control. Clean production scraps can sometimes be separated, tested, and reused without weakening product quality. Contaminated waste requires careful storage and documented disposal through authorized channels. Cooling water may circulate in a closed system, reducing freshwater consumption. Filters and treatment units help control suspended solids before discharge. Air emissions also need regular monitoring, not occasional checking. Independent laboratory testing can verify product safety and environmental performance. No system is perfect. Operators may overlook a blocked filter or rely too heavily on old inspection records. Honest reporting, corrective actions, and periodic external audits make improvement more credible. A responsible PVC factory measures energy, water, scrap, emissions, and incidents over time, then adjusts equipment and training based on evidence.
